
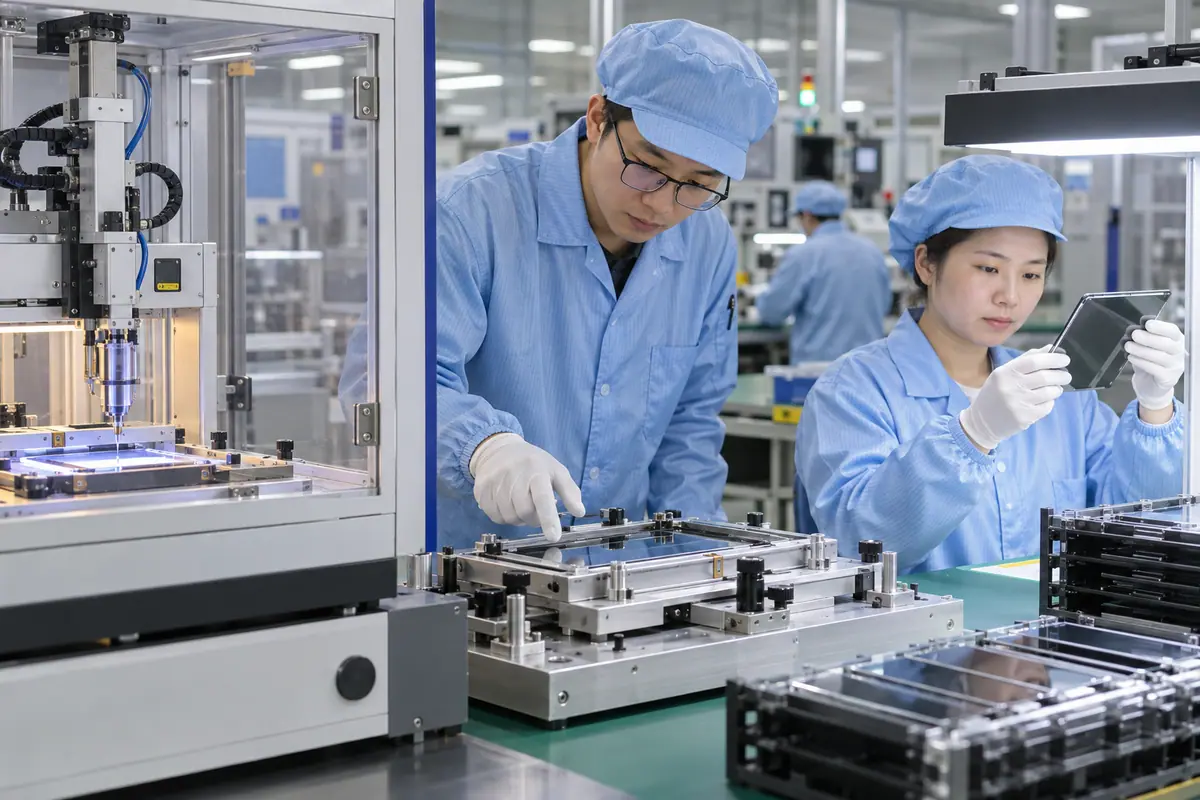
Choosing a touchscreen optical bonding manufacturer is a process-audit decision as much as a purchasing decision. The supplier may join customer-owned components, inspect a defined optical interface or deliver a wider module. This guide focuses on the joining service: incoming condition, preparation, alignment, material control, inspection and loss ownership. Ask for evidence from the proposed construction rather than treating equipment photographs or a general factory introduction as proof of repeatable output.
Contents: 1 · 2 · 3 · 4 · 5 · 6 · 7 · 8 · 9 · 10
1. What joining service is actually included?
List the parts supplied by each party and the interfaces the manufacturer will join. Also, distinguish optical processing from controller integration and finished-module testing. Contract joining can have a narrower boundary than complete-screen supply. A shared scope prevents purchasing from comparing a process fee with an offer that includes additional components or engineering.
Missing scope can leave test ownership unresolved. Customer-part loss may be excluded from a seemingly attractive joining quotation.
Buyer checklist for touchscreen optical bonding manufacturer
Define the processing contract. Attach an interface section and supplied-parts list to the RFQ. Require clear exclusions and ownership terms, then compare quotes only after each supplier acknowledges the same joining and inspection boundary.
- Joined interfaces
- Supplied parts
- Excluded work
- Loss ownership
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Missing scope can leave test ownership unresolved. Customer-part loss may be excluded from a seemingly attractive joining quotation. | Excluded work |
| Approval action | Attach an interface section and supplied-parts list to the RFQ. Require clear exclusions and ownership terms, then compare quotes only after each supplier acknowledges the same joining and inspection boundary. | Loss ownership |
Review public supplier information alongside evidence for the actual part being quoted. factory background.
2. How are incoming customer parts accepted?
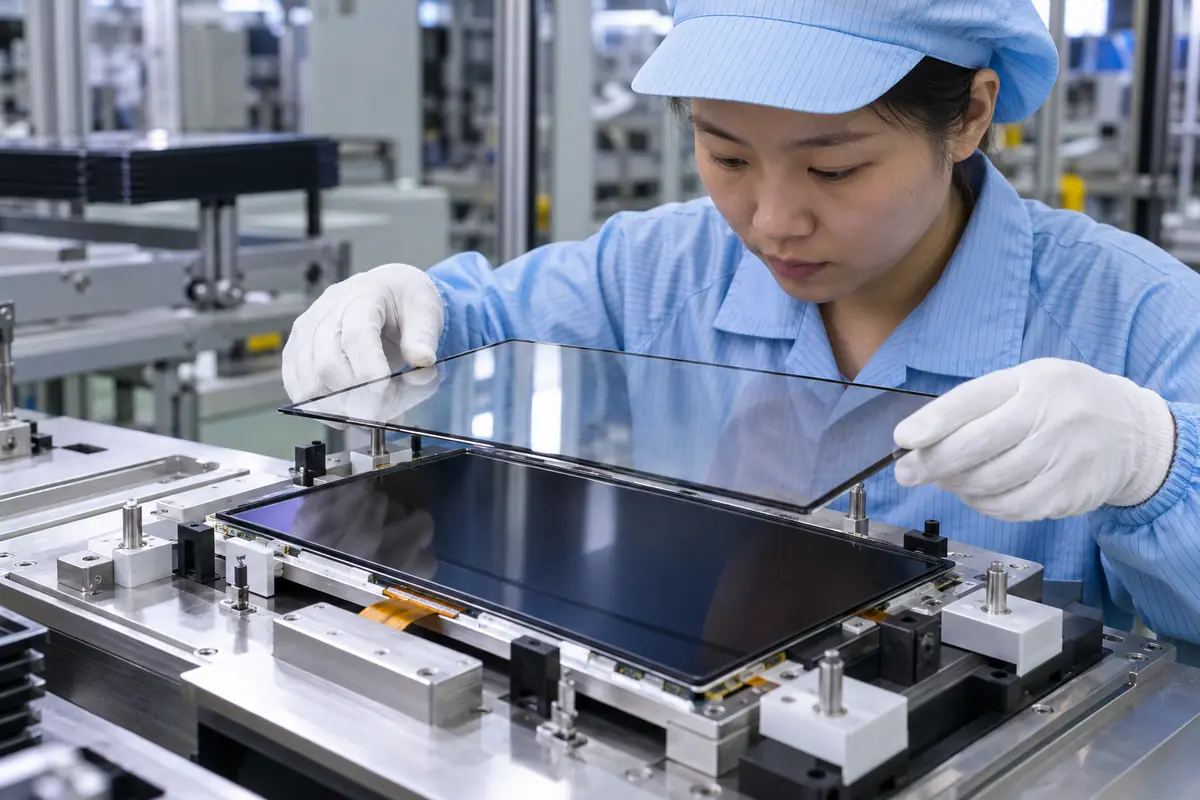
Cover surfaces, LCD condition, dimensions and identifiers should be reviewed before processing. Meanwhile, packaging and prior handling can introduce defects that later appear inside a joined stack. Define how incoming exceptions are recorded and authorized. A final reject is difficult to investigate when no one documented the condition of the unprocessed parts.
A pre-existing scratch can be mistaken for process damage. Unidentified incoming lots can obstruct traceability and fair loss allocation.
Which evidence should accompany the sample?
Record the starting condition. Agree on incoming inspection and exception records with quality owners. Retain part and lot links, then require disposition of nonconforming incoming material before the manufacturer proceeds with joining.
- Surface condition
- Part identity
- Lot linkage
- Exception approval
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A pre-existing scratch can be mistaken for process damage. Unidentified incoming lots can obstruct traceability and fair loss allocation. | Lot linkage |
| Approval action | Agree on incoming inspection and exception records with quality owners. Retain part and lot links, then require disposition of nonconforming incoming material before the manufacturer proceeds with joining. | Exception approval |
Send the controlled drawing and unresolved test questions with the sample configuration attached. technical inquiry route.
3. Which preparation controls should the audit examine?
Review handling, cleaning, exposed-surface protection and the transition into joining. The method should suit coatings, borders and display surfaces. Also, operator practice matters alongside the environment. A room classification or photograph provides context but does not establish that the proposed part receives a controlled preparation and inspection sequence.
An unsuitable cleaning method can damage parts. A clean-looking facility may still allow contamination during an uncontrolled transfer step.
What should the test owner record?
Audit the part's handling path. Ask the process owner to demonstrate representative preparation and protection steps. Review relevant records and inspection responsibility, then investigate observed pilot defects against the actual sequence rather than the facility label.
- Cleaning compatibility
- Surface protection
- Transfer steps
- Inspection owner
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An unsuitable cleaning method can damage parts. A clean-looking facility may still allow contamination during an uncontrolled transfer step. | Transfer steps |
| Approval action | Ask the process owner to demonstrate representative preparation and protection steps. Review relevant records and inspection responsibility, then investigate observed pilot defects against the actual sequence rather than the facility label. | Inspection owner |
Module quotes need a defined LCD, sensor and controller boundary. touch display module scope.
Primary reference: 3M optically clear adhesive application context. Verify its applicable scope against the proposed build.
4. How are alignment and fixtures controlled?
Fixtures should reference the required opening, border and tail clearances. Meanwhile, part tolerances and different revisions can change fit. Ask how the factory prevents a similar but incorrect component from entering the setup. An impressive machine does not establish that its fixture, recipe and inspection references match the proposed assembly.
An outdated fixture can create systematic offset. A misrouted tail can be damaged without an obvious front-view defect.
Which installed detail needs approval?
Link fixtures to drawings. Review fixture identity, setup approval and alignment inspection against the controlled drawing. Observe a representative build, then retain revision and change rules for tooling that affects the accepted joining geometry.
- Datum references
- Fixture identity
- Tail clearance
- Setup approval
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An outdated fixture can create systematic offset. A misrouted tail can be damaged without an obvious front-view defect. | Tail clearance |
| Approval action | Review fixture identity, setup approval and alignment inspection against the controlled drawing. Observe a representative build, then retain revision and change rules for tooling that affects the accepted joining geometry. | Setup approval |
Review the capacitive product context if glass-front or gesture operation enters the specification. capacitive touchscreen options.
5. What proves optical material control?
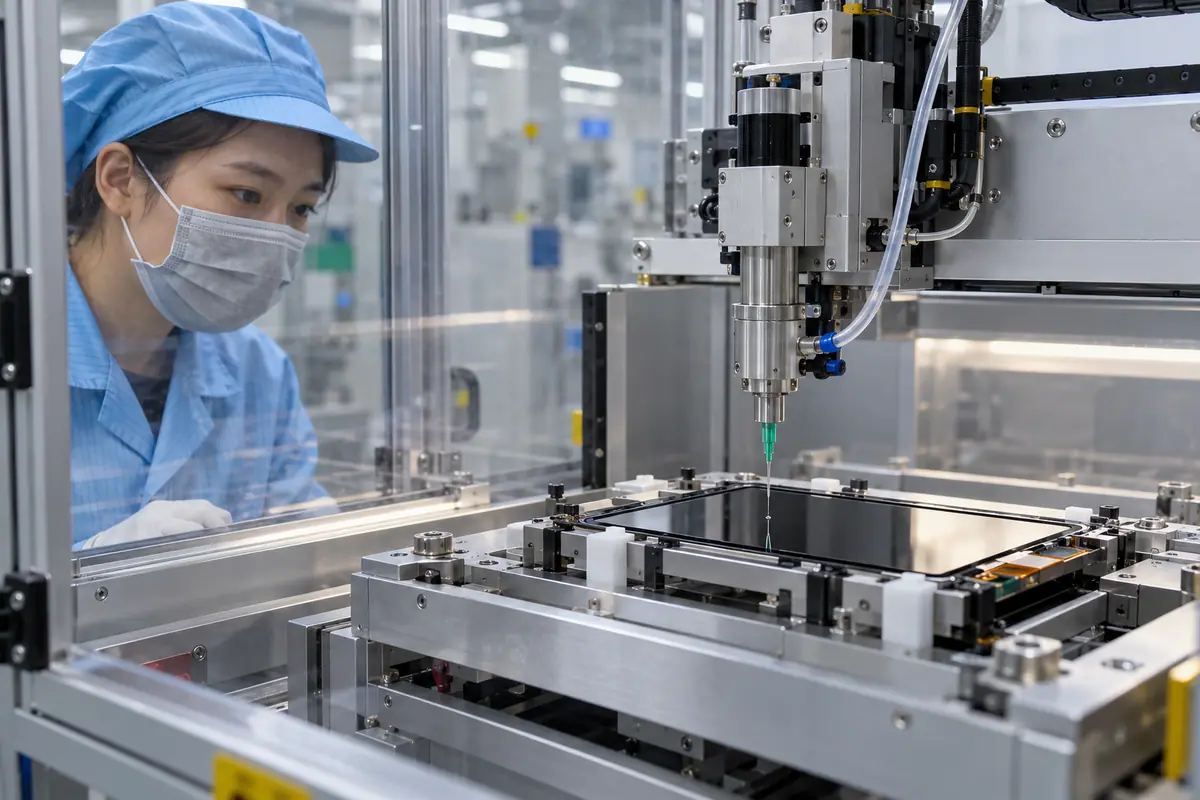
Request exact material references and relevant storage, handling and traceability controls. Also, distinguish approved alternatives from unreviewed substitutes. The process should follow applicable material guidance and component constraints. A brand name on a brochure does not establish which product, lot or construction entered the pilot or repeat-production assembly.
An unrecorded substitution can alter process behavior. Expired or mishandled material can make nominally identical builds difficult to compare.
How can engineering close this check?
Track the actual optical material. Connect incoming material identity to the build record and approved route. Review relevant handling controls with the process owner, then require notice and proportionate evidence before accepting alternative materials.
- Product identity
- Lot reference
- Handling control
- Alternative approval
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An unrecorded substitution can alter process behavior. Expired or mishandled material can make nominally identical builds difficult to compare. | Handling control |
| Approval action | Connect incoming material identity to the build record and approved route. Review relevant handling controls with the process owner, then require notice and proportionate evidence before accepting alternative materials. | Alternative approval |
Use the pressure-input product context when a suitable blunt stylus or glove is required. resistive touchscreen options.
6. How should liquid or film process evidence differ?
A film route needs applicable liner, contact and alignment controls. A liquid route needs applicable dispensing, containment and curing or setting controls. Meanwhile, both need defined output inspection. Review the route actually quoted rather than demanding a generic checklist that overlooks the critical step for that material and geometry.
A film-focused audit can miss liquid flow or cure issues. A liquid checklist may ignore film shape and liner-handling defects.
What failure would reject this configuration?
Audit the selected route. Ask the supplier to map the proposed process and critical output checks. Review representative records and failure response, then align the audit evidence with the material-specific route and proposed stack.
- Material form
- Critical steps
- Output checks
- Failure response
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A film-focused audit can miss liquid flow or cure issues. A liquid checklist may ignore film shape and liner-handling defects. | Output checks |
| Approval action | Ask the supplier to map the proposed process and critical output checks. Review representative records and failure response, then align the audit evidence with the material-specific route and proposed stack. | Failure response |
A bonding proposal changes the assembled optical and mechanical interface; review its construction context. fully laminated touchscreen construction.
7. How are defects judged and contained?
Agree on relevant optical and dimensional limits using a reproducible inspection setup. Also, separate cosmetic defects from functional failures and customer-part issues. The manufacturer should show how nonconforming parts are identified and prevented from mixing with accepted output. A favorable sample photograph does not establish repeat-production disposition control.
Inconsistent viewing conditions can cause acceptance disputes. Uncontrolled rework can return a changed assembly without renewed inspection.
What should quality retain?
Follow defects through disposition. Review inspection conditions, reject identification and disposition authority. Retain pilot defect records and corrective actions, then require reinspection and traceability for any approved rework before releasing the affected assembly.
- Inspection method
- Reject segregation
- Rework authority
- Release record
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Inconsistent viewing conditions can cause acceptance disputes. Uncontrolled rework can return a changed assembly without renewed inspection. | Rework authority |
| Approval action | Review inspection conditions, reject identification and disposition authority. Retain pilot defect records and corrective actions, then require reinspection and traceability for any approved rework before releasing the affected assembly. | Release record |
For a machine installation, relate these checks to mounted-console and operator conditions. industrial control touchscreen context.
8. What pilot evidence demonstrates repeatability?
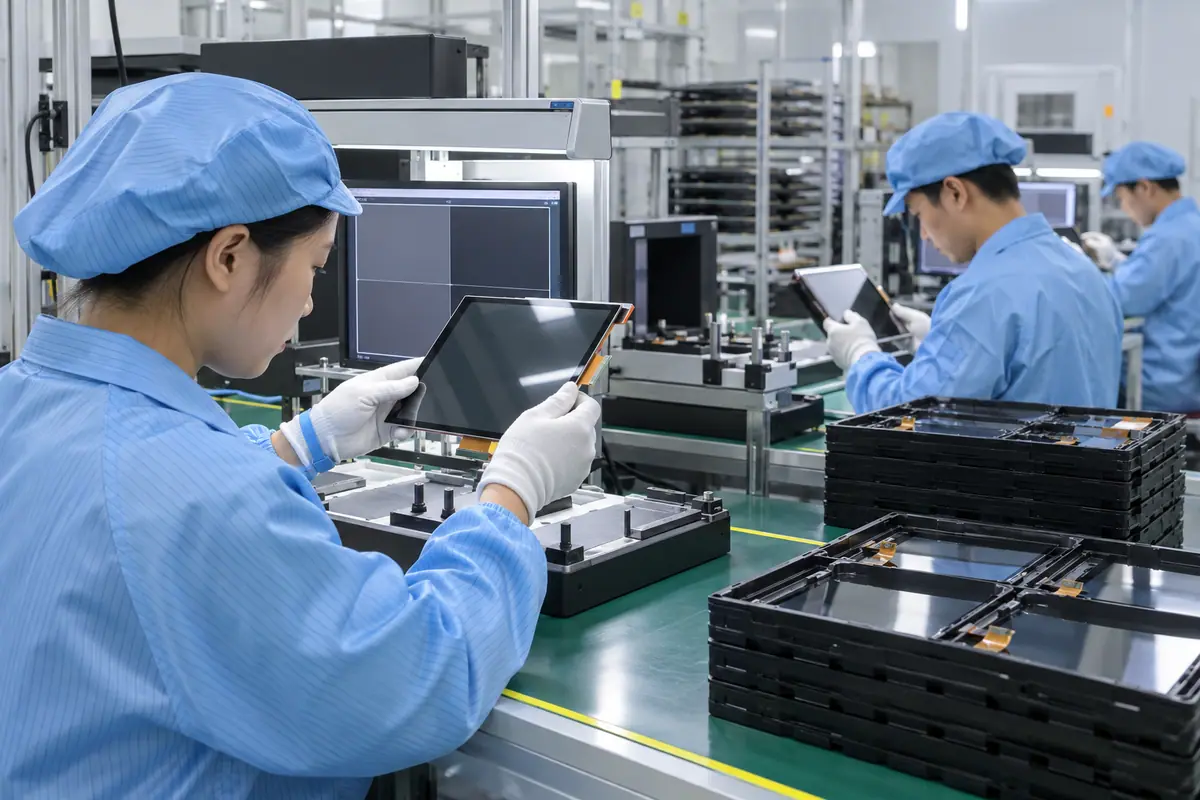
Request an identified production-intent build with the agreed route and inspection records. Feasibility samples can be useful but may contain special handling or nonstandard parts. Meanwhile, a yield statement needs its scope and conditions to be interpretable. Avoid treating an unsupported percentage or a single excellent sample as a production capability guarantee.
Special sample treatment may not represent routine processing. A broad yield claim can conceal incoming exclusions or different product geometry.
Which trial result changes the decision?
Distinguish pilot evidence from promises. Record pilot configuration, deviations and observed results. Compare evidence with the proposed production route, then close unresolved process risks and loss terms before relying on the offer for repeat supply.
- Build identity
- Route match
- Deviation record
- Observed outcomes
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Special sample treatment may not represent routine processing. A broad yield claim can conceal incoming exclusions or different product geometry. | Deviation record |
| Approval action | Record pilot configuration, deviations and observed results. Compare evidence with the proposed production route, then close unresolved process risks and loss terms before relying on the offer for repeat supply. | Observed outcomes |
Healthcare equipment introduces device-specific cleaning and qualification questions; keep those outside generic component claims. medical touchscreen context.
For example, an OEM may send LCDs for contract joining and later find visible edge marks on rejected units. Compare incoming photographs and inspection records before allocating loss. Then identify whether handling, alignment or another stage introduced the change and agree on a corrective pilot. This hypothetical audit path is more useful than assuming either party is responsible without evidence.
9. What commercial terms should the process audit inform?
Material consumption, setup, fixtures, inspection, scrap and customer-part exposure can enter the offer differently. Also, rework and replacement obligations may be conditional. Engineering and purchasing should reconcile these terms with actual process evidence. A low joining fee does not identify the full accepted-output cost or the owner of an unsuccessful pilot.
Unclear reject ownership can outweigh a nominal fee saving. Unpriced inspection or tooling can emerge after parts arrive at the factory.
How can purchasing compare the evidence?
Compare accepted-output responsibility. Normalize included deliverables and loss-allocation terms in one comparison. Ask for explicit exceptions and change charges, then reconcile pilot findings and commercial scope before authorizing processing of customer-owned components.
- Setup scope
- Inspection inclusion
- Scrap owner
- Change charges
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Unclear reject ownership can outweigh a nominal fee saving. Unpriced inspection or tooling can emerge after parts arrive at the factory. | Scrap owner |
| Approval action | Normalize included deliverables and loss-allocation terms in one comparison. Ask for explicit exceptions and change charges, then reconcile pilot findings and commercial scope before authorizing processing of customer-owned components. | Change charges |
Compare the application boundary before assuming a single demonstration covers every installation. application solution overview.
10. What defines an approved bonding manufacturer?
Approval should name the construction, process route, inspection boundary and commercial responsibility actually reviewed. Keep critical open items visible. By contrast, touchscreen optical bonding manufacturer is a sourcing category, not evidence of every capability. A different material, fixture or customer part may need a fresh process review even at the same facility.
Factory-level approval can be misapplied to an untested stack. A silent route change can break the link to accepted pilot evidence.
What should the team release next?
Approve a defined process scope. Release the supplier against controlled process and part references. Require relevant notices and records, then review affected alignment, optical, functional and loss-ownership questions before approving a revised route or construction.
- Part references
- Process route
- Inspection boundary
- Change review
Frequently asked questions about touchscreen optical bonding manufacturer
Q1: Is a cleanroom photograph enough to approve the supplier? No. Review the proposed part's handling route, process controls, inspection and traceability evidence.
Q2: Who should own customer-supplied part damage? Agree on incoming condition, process loss and disposition responsibility before processing begins.
Q3: Should film and liquid routes use identical audit checklists? Share output requirements but examine the route-specific critical steps and evidence.
Q4: Can one excellent sample prove routine yield? No. Request identified pilot results, scope and deviations without treating unsupported percentages as guarantees.
Q5: What should supplier approval reference? The accepted construction, route, inspection boundary, records and change-notification rules.