
Fully laminated vs air gap display selection changes product architecture, assembly ownership and field repair. A joined optical stack and an intentionally spaced construction can both be valid when their remaining risks fit the application. This guide compares complete delivery and service boundaries, not just adhesive physics. It helps an OEM conduct an equal-scope sample trial and cost review without claiming that lamination always wins or that an air gap is automatically inferior.
Contents: 1 · 2 · 3 · 4 · 5 · 6 · 7 · 8 · 9 · 10
1. Which complete constructions are being compared?
Define the LCD, cover, sensor, supports and electronics for both options. An air-gap assembly intentionally retains spacing at a specified interface. Meanwhile, a laminated product should identify which surfaces are joined. Compare cross-sections rather than labels because either supplier may exclude different layers or integration work.
A narrow stack quote and a complete display quote are not equivalent. Unnamed interfaces make later fault ownership unclear.
Buyer checklist for fully laminated vs air gap display
Compare defined architectures. Draw both proposed assemblies on shared datums and mark supplied functions. Reconcile quotations with those constructions, then compare only deliberate architectural differences and explicit exclusions.
- Joined interfaces
- Spaced interfaces
- Delivered layers
- Integration owner
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A narrow stack quote and a complete display quote are not equivalent. Unnamed interfaces make later fault ownership unclear. | Delivered layers |
| Approval action | Draw both proposed assemblies on shared datums and mark supplied functions. Reconcile quotations with those constructions, then compare only deliberate architectural differences and explicit exclusions. | Integration owner |
Review public supplier information alongside evidence for the actual part being quoted. factory background.
2. How should visible performance be compared fairly?
Keep required content, illumination and useful brightness settings consistent. Joining can reduce reflections at an addressed air interface, but other optical differences remain. Also, coatings and LCD selection can dominate appearance. Compare complete modules from the actual viewing positions rather than unrelated photographs or unmatched panel technologies.
A different cover or backlight setting can distort the result. Neither label guarantees sunlight visibility or an unsourced contrast improvement.
Which evidence should accompany the sample?
Hold visual variables steady. Record every optical difference and test equivalent operating settings. Inspect required content and remaining glare, then decide whether the measured visual benefit addresses a mandatory task or a preference.
- Common LCD conditions
- Front finish
- Ambient light
- Required content
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A different cover or backlight setting can distort the result. Neither label guarantees sunlight visibility or an unsourced contrast improvement. | Ambient light |
| Approval action | Record every optical difference and test equivalent operating settings. Inspect required content and remaining glare, then decide whether the measured visual benefit addresses a mandatory task or a preference. | Required content |
Send the controlled drawing and unresolved test questions with the sample configuration attached. technical inquiry route.
3. What mechanical work does each option require?
Air-gap products need controlled spacers, edge support and clearance. Laminated stacks need suitable layer support and reviewed stress transfer. Meanwhile, both still depend on enclosure datums and fastening. A stronger-looking joined front can load an LCD improperly. A spaced design can permit contact marks if its gap collapses.
Poor supports can defeat either architecture. Identical outside dimensions do not prove equivalent installed behavior under mounting loads.
What should the test owner record?
Include the mounting architecture. Review both fitted cross-sections with mechanical staff. Check clearances, support and image appearance after fastening, then validate the actual assembly rather than approving either construction loose on a bench.
- Gap control
- Layer support
- Fastening loads
- Fitted appearance
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Poor supports can defeat either architecture. Identical outside dimensions do not prove equivalent installed behavior under mounting loads. | Fastening loads |
| Approval action | Review both fitted cross-sections with mechanical staff. Check clearances, support and image appearance after fastening, then validate the actual assembly rather than approving either construction loose on a bench. | Fitted appearance |
Module quotes need a defined LCD, sensor and controller boundary. touch display module scope.
Primary reference: 3M optically clear adhesive application context. Verify its applicable scope against the proposed build.
4. How do dust and moisture questions differ?
A joined interface removes an intentional cavity at that location, while a spaced assembly needs a suitable contamination strategy. However, seals, rear connectors and cable entries remain separate. Internal optical contamination and enclosure ingress protection need different evidence. Do not transfer an unrelated rating or assume that filling one interface seals the whole device.
A gap can collect visible contamination if its protection fails. A laminated front can still leave unprotected housing or cable paths.
Which installed detail needs approval?
Separate cavity control from sealing. Define contamination and ingress boundaries for each complete product. Test relevant optical and sealing conditions separately, then keep qualified reports tied to the exact enclosure and stack being considered.
- Optical cavity
- Edge protection
- Housing joints
- Applicable seal evidence
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A gap can collect visible contamination if its protection fails. A laminated front can still leave unprotected housing or cable paths. | Housing joints |
| Approval action | Define contamination and ingress boundaries for each complete product. Test relevant optical and sealing conditions separately, then keep qualified reports tied to the exact enclosure and stack being considered. | Applicable seal evidence |
Review the capacitive product context if glass-front or gesture operation enters the specification. capacitive touchscreen options.
5. How does touch integration change?
A changed joining layer or distance can alter capacitive conditions. A pressure-sensitive assembly needs a construction designed for its required movement. Also, surrounding metal and LCD activity belong in either fitted trial. A sensor qualified in one architecture should not automatically retain acceptance after moving to the other.
Existing tuning or calibration may not cover the changed stack. A mounting fault can be mistaken for a technology limitation.
How can engineering close this check?
Retest the input combination. Test named input objects with the actual LCD, host and enclosure. Record raw and mapped behavior, then repeat relevant edge, release and idle checks after the architecture or joining arrangement changes.
- Sensor mechanism
- Joining change
- Final host
- Edge behavior
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Existing tuning or calibration may not cover the changed stack. A mounting fault can be mistaken for a technology limitation. | Final host |
| Approval action | Test named input objects with the actual LCD, host and enclosure. Record raw and mapped behavior, then repeat relevant edge, release and idle checks after the architecture or joining arrangement changes. | Edge behavior |
Use the pressure-input product context when a suitable blunt stylus or glove is required. resistive touchscreen options.
6. Which repair boundary suits the service plan?
Separate layers can sometimes support localized replacement, depending on access and materials. A joined stack may require specialist rework or a larger spare. Meanwhile, neither arrangement guarantees cheap service. Ask maintenance staff to demonstrate the actual route. Include mapping checks and optical inspection after repair, not only removal of a failed front part.
A theoretically replaceable layer may be inaccessible. Assumed recovery of a bonded LCD can underestimate scrap and labor.
What failure would reject this configuration?
Let service test the alternatives. Define the replaceable unit, tools and post-repair tests for both options. Demonstrate service on fitted samples, then compare spare scope and downtime assumptions with the responsible service team.
- Replaceable unit
- Required tools
- Rework boundary
- Recovery checks
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A theoretically replaceable layer may be inaccessible. Assumed recovery of a bonded LCD can underestimate scrap and labor. | Rework boundary |
| Approval action | Define the replaceable unit, tools and post-repair tests for both options. Demonstrate service on fitted samples, then compare spare scope and downtime assumptions with the responsible service team. | Recovery checks |
A bonding proposal changes the assembled optical and mechanical interface; review its construction context. fully laminated touchscreen construction.
7. What manufacturing risks belong in each quote?
Air-gap assembly can require spacing, sealing and internal cleanliness controls. Full-area joining can introduce alignment, particle, bubble and process-control questions. Also, customer-supplied parts need explicit reject handling. Compare the operations each factory owns. A smaller recurring price may omit joining or final inspection rather than reflect a better controlled process.
Unpriced assembly work can move into the OEM line. Undefined defect criteria can create disputes after pilot deliveries.
What should quality retain?
Compare process responsibilities. Ask both suppliers for production scope and applicable inspection methods. Normalize supplied-part and reject responsibilities, then compare pilot results against shared acceptance criteria before approving either manufacturing route.
- Spacing control
- Joining control
- Inspection scope
- Reject ownership
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Unpriced assembly work can move into the OEM line. Undefined defect criteria can create disputes after pilot deliveries. | Inspection scope |
| Approval action | Ask both suppliers for production scope and applicable inspection methods. Normalize supplied-part and reject responsibilities, then compare pilot results against shared acceptance criteria before approving either manufacturing route. | Reject ownership |
For a machine installation, relate these checks to mounted-console and operator conditions. industrial control touchscreen context.
8. How should lifecycle cost be normalized?
Include components, fixtures, joining or spacing work, qualification and service. Meanwhile, separate one-time engineering from recurring purchases. Use the same quantities and commercial basis. A direct comparison of a loose panel with a joined module hides remaining work. Avoid universal price ranges or invented failure rates; label planning assumptions explicitly.
Different volume or repair assumptions can reverse an apparent saving. Double-counted tooling can distort a lifecycle total.
Which trial result changes the decision?
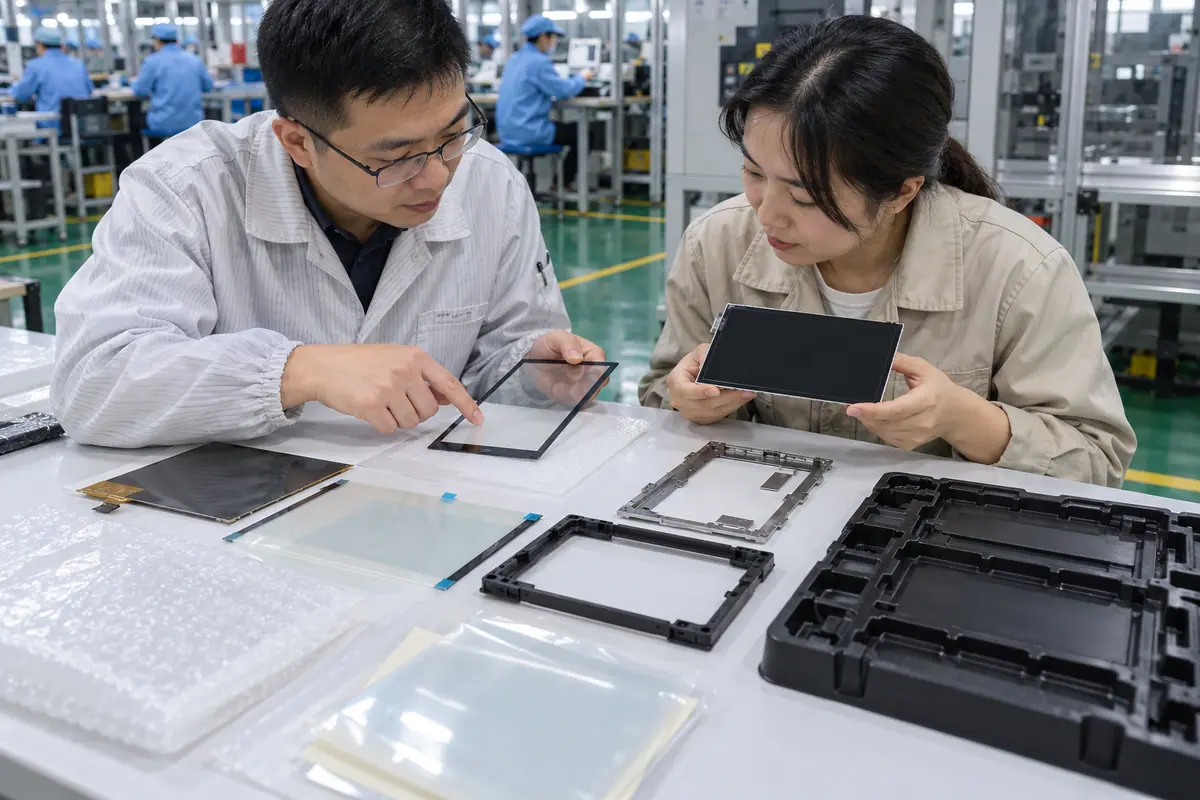
Price equal delivered functions. Build one traceable equal-scope calculation using dated offers. Review uncertain assembly and service inputs, then compare sensitivity to accepted quantity and replacement policy before choosing the architecture.
- Recurring scope
- Nonrecurring work
- Accepted quantity
- Service assumptions
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Different volume or repair assumptions can reverse an apparent saving. Double-counted tooling can distort a lifecycle total. | Accepted quantity |
| Approval action | Build one traceable equal-scope calculation using dated offers. Review uncertain assembly and service inputs, then compare sensitivity to accepted quantity and replacement policy before choosing the architecture. | Service assumptions |
Healthcare equipment introduces device-specific cleaning and qualification questions; keep those outside generic component claims. medical touchscreen context.
For example, a service terminal may compare a spaced display that is easy to repair with a bonded alternative that reads better under required light. Test both on the same host and with approved gloves. Then demonstrate replacement and price the actual spare. If the optical benefit meets a mandatory condition, retain its service consequence explicitly. This hypothetical decision does not claim that either architecture always has lower total cost.
9. What trial should settle the comparison?
Run required visual and input tasks on production-intent assemblies. Include fitted geometry, relevant exposure and normal recovery states. For example, a glare improvement may have little value if a required glove task fails. Also, observe retries and service access. Keep mandatory pass-fail gates separate from weighted appearance preferences.
A favorable average can conceal failure of one required task. A temporary fixture may hide the final mechanical difference.
How can purchasing compare the evidence?
Gate mandatory tasks before preference. Agree on one comparison plan with responsible task owners. Retain failed conditions and corrective revisions, then shortlist only configurations meeting required operating and service boundaries or explicitly approved product changes.
- Required visibility
- Required input
- Installed exposure
- Service access
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A favorable average can conceal failure of one required task. A temporary fixture may hide the final mechanical difference. | Installed exposure |
| Approval action | Agree on one comparison plan with responsible task owners. Retain failed conditions and corrective revisions, then shortlist only configurations meeting required operating and service boundaries or explicitly approved product changes. | Service access |
Compare the application boundary before assuming a single demonstration covers every installation. application solution overview.
10. Which architecture should enter the order?
Select the construction whose demonstrated benefits justify its integration and service consequences. A suitable air-gap assembly may fit a repair-led project. A validated laminated stack may fit a defined optical requirement. By contrast, neither label substitutes for acceptance evidence. Release the actual component and mounting combination rather than a universal technology preference.
A generic order can hide unqualified variants. Later cover, adhesive or spacer changes can invalidate the accepted comparison.
What should the team release next?
Release the tested architecture. Approve the tested architecture and equal-scope offer together. Freeze cross-section, interfaces and test methods, then require affected-interface review for material, support, controller or service-boundary changes.
- Accepted construction
- Controlled interfaces
- Comparison evidence
- Change triggers
Frequently asked questions about fully laminated vs air gap display
Q1: Is full lamination always the better choice? No. Required visibility, integration, service and evidence should determine the specific architecture.
Q2: Can an air-gap construction be appropriate? Yes, when its spacing, cleanliness, protection and operating tasks are suitably controlled and validated.
Q3: Does either option establish an ingress rating? No. Qualify the applicable assembled enclosure and retain report scope.
Q4: What makes quotations comparable? Equivalent supplied components, assembly work, tests, quantities and service responsibilities.
Q5: What should settle a close choice? A controlled fitted trial plus a transparent lifecycle comparison of technically viable configurations.