
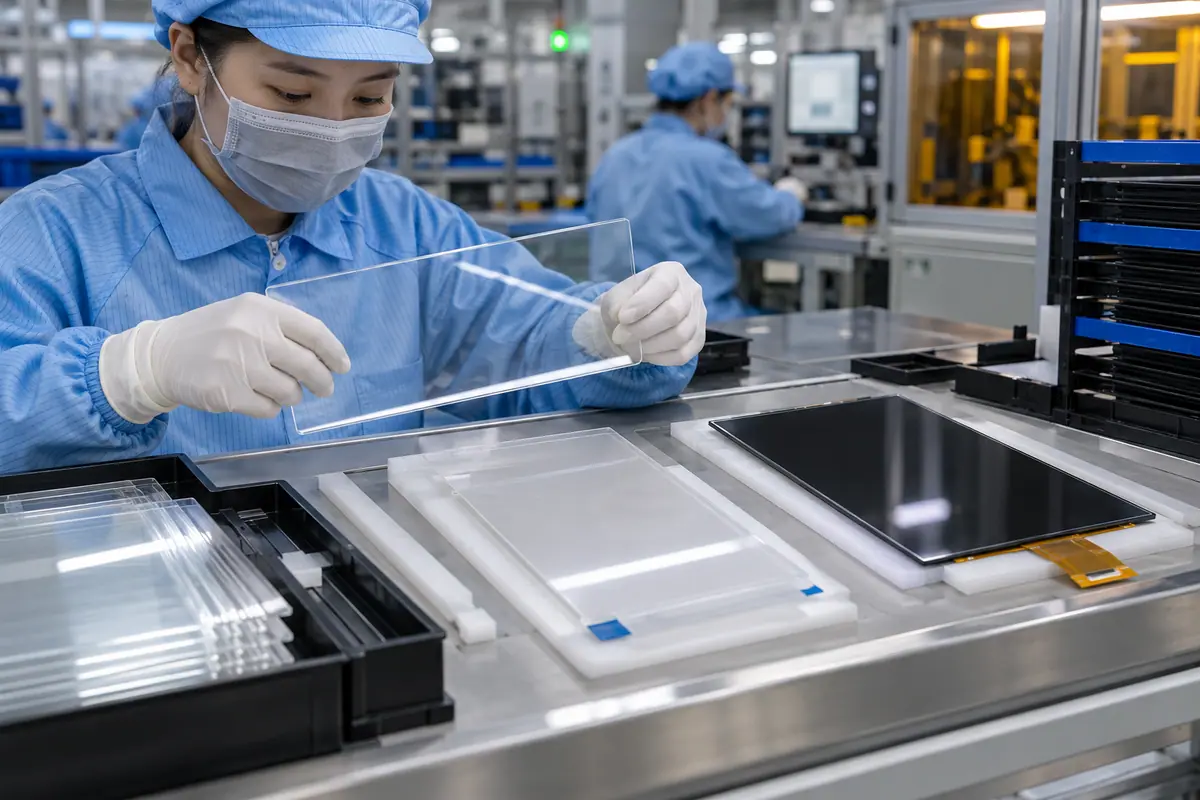
What is optical bonding in a display project? It is an optical joining approach that replaces a selected air interface with a suitable transparent coupling material. The exact surfaces, material form and process vary by construction. This guide explains the mechanism and the decisions it creates for an OEM buyer. It distinguishes process terminology from complete-module performance so a material claim does not become an unsupported promise about every finished touchscreen.
Contents: 1 · 2 · 3 · 4 · 5 · 6 · 7 · 8 · 9 · 10
1. Which interface is being optically joined?
Ask for a cross-section naming the cover, sensor, display and proposed joined surfaces. Some stacks contain more than one interface, and not all must use the same construction. Also, distinguish optical coupling across the viewing area from a perimeter attachment that retains an air gap. The process label alone cannot identify the actual proposal.
An ambiguous cross-section can hide an untreated gap. Two suppliers may use the same term for different assembly boundaries.
Buyer checklist for what is optical bonding
Name the joined surfaces. Mark the surfaces and joining region on a controlled section. Identify remaining gaps and excluded work, then align the quote and sample inspection with the construction the OEM actually intends to evaluate.
- Stack layers
- Joining region
- Remaining gaps
- Delivery scope
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An ambiguous cross-section can hide an untreated gap. Two suppliers may use the same term for different assembly boundaries. | Remaining gaps |
| Approval action | Mark the surfaces and joining region on a controlled section. Identify remaining gaps and excluded work, then align the quote and sample inspection with the construction the OEM actually intends to evaluate. | Delivery scope |
Healthcare equipment introduces device-specific cleaning and qualification questions; keep those outside generic component claims. medical touchscreen context.
2. Why can replacing an air interface change reflections?
Light encounters boundaries between materials with different optical properties. A suitable coupling material can reduce reflection associated with the addressed internal air interface. Meanwhile, front-surface reflection, display behavior and viewing geometry remain. The useful result therefore belongs to the complete stack under defined conditions, not to the adhesive name alone.
A single-interface benefit does not guarantee readable content. Unmatched brightness or cover finishes can obscure the cause of an observed improvement.
Which evidence should accompany the sample?
Connect the mechanism to a task. Compare complete samples using equivalent settings and viewing conditions. Separate internal-reflection goals from other glare sources, then judge the required content rather than extrapolating from a material transmission figure.
- Interface properties
- Outer glare
- Matched settings
- Readable content
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A single-interface benefit does not guarantee readable content. Unmatched brightness or cover finishes can obscure the cause of an observed improvement. | Matched settings |
| Approval action | Compare complete samples using equivalent settings and viewing conditions. Separate internal-reflection goals from other glare sources, then judge the required content rather than extrapolating from a material transmission figure. | Readable content |
Compare the application boundary before assuming a single demonstration covers every installation. application solution overview.
3. What material forms may be proposed?
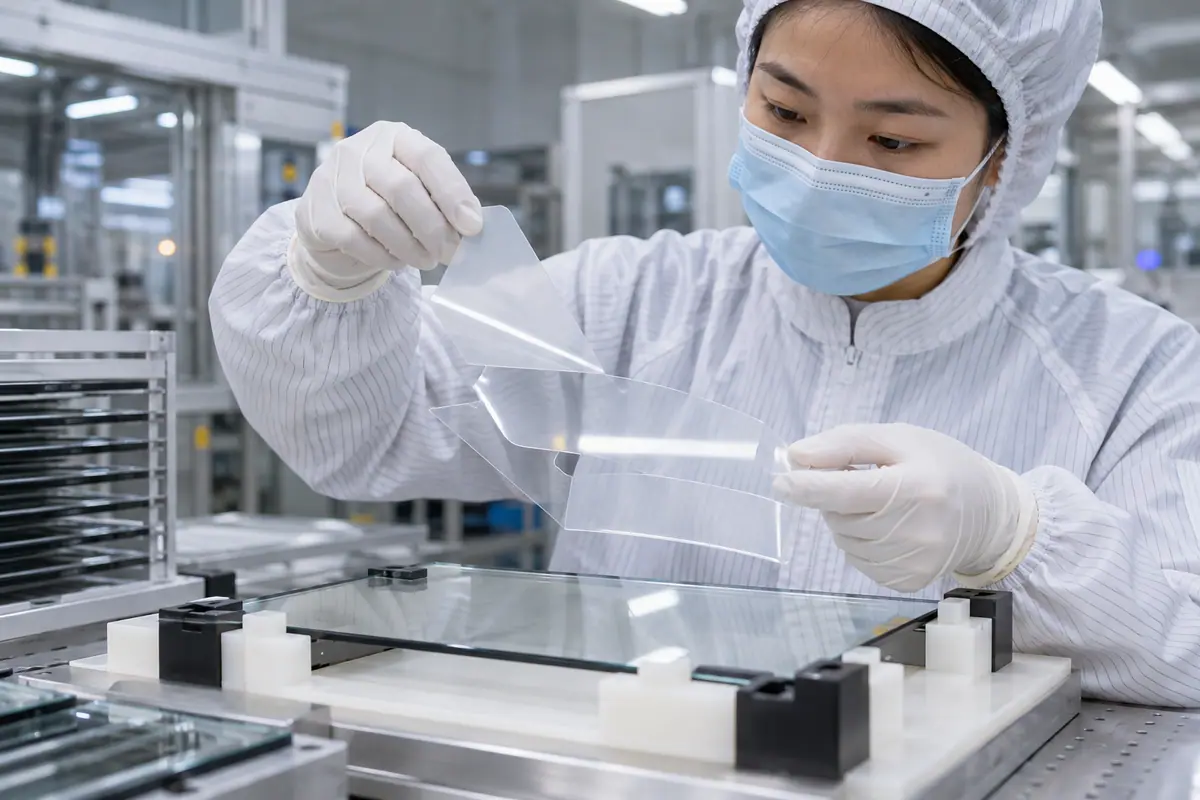
Optical joining can use suitable solid films, liquid systems or other qualified coupling approaches. Material form affects handling and processing but does not alone define the best choice. Also, the exact chemistry, thickness and compatibility matter. Review the proposal against geometry, surfaces, equipment and required evidence rather than accepting a universal material ranking.
A broad acronym can conceal different products and processes. A datasheet for one formulation may not apply to a proposed substitute.
What should the test owner record?
Identify the actual material. Request exact material references and applicable technical guidance. Ask the process owner to explain fit to the proposed stack, then compare sample evidence and exclusions before selecting a route.
- Material form
- Product reference
- Stack compatibility
- Process rationale
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A broad acronym can conceal different products and processes. A datasheet for one formulation may not apply to a proposed substitute. | Stack compatibility |
| Approval action | Request exact material references and applicable technical guidance. Ask the process owner to explain fit to the proposed stack, then compare sample evidence and exclusions before selecting a route. | Process rationale |
Review public supplier information alongside evidence for the actual part being quoted. factory background.
Primary reference: 3M optically clear adhesive application context. Verify its applicable scope against the proposed build.
4. How does surface preparation affect the result?
Particles, residue and handling marks can interfere with a clean optical interface. Meanwhile, different surfaces may require different approved preparation. The cleaning method should preserve coatings, printing and display surfaces. A cleanroom description is useful context but does not replace process records, inspection limits or evidence that the actual parts were prepared correctly.
Aggressive preparation can damage a surface before joining. A visually clean work area does not establish a defect-free accepted bond.
Which installed detail needs approval?
Control the starting surfaces. Ask for relevant preparation and handling controls with inspection responsibility. Evaluate representative parts and record approved deviations, then connect observed defects to the actual process stage rather than blaming material form alone.
- Incoming condition
- Preparation method
- Handling controls
- Inspection responsibility
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Aggressive preparation can damage a surface before joining. A visually clean work area does not establish a defect-free accepted bond. | Handling controls |
| Approval action | Ask for relevant preparation and handling controls with inspection responsibility. Evaluate representative parts and record approved deviations, then connect observed defects to the actual process stage rather than blaming material form alone. | Inspection responsibility |
Send the controlled drawing and unresolved test questions with the sample configuration attached. technical inquiry route.
5. What does the joining step need to control?
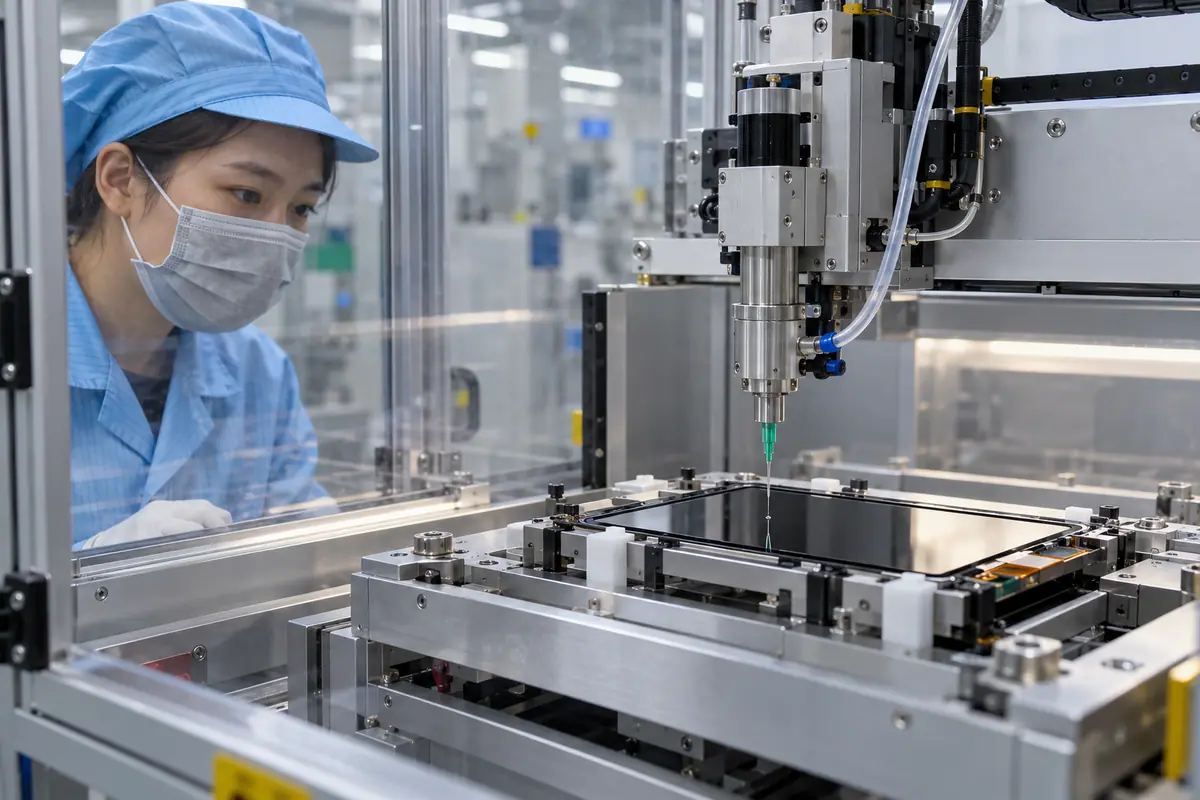
Alignment, contact progression and material distribution depend on the selected route. Also, process conditions must suit the parts and material guidance. Do not invent a pressure, temperature or cure recipe from the term optical bonding. The supplier should demonstrate a controlled route that produces the agreed optical and dimensional output without damaging the stack.
Poor alignment can obscure the display opening. An unsuitable process can create voids or stress even when the adhesive itself is appropriate.
How can engineering close this check?
Judge a controlled process output. Review the proposed process boundary and critical output checks. Request a representative build record and sample inspection, then let qualified process owners establish settings within applicable material and component limits.
- Alignment reference
- Material distribution
- Component limits
- Build record
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Poor alignment can obscure the display opening. An unsuitable process can create voids or stress even when the adhesive itself is appropriate. | Component limits |
| Approval action | Review the proposed process boundary and critical output checks. Request a representative build record and sample inspection, then let qualified process owners establish settings within applicable material and component limits. | Build record |
Module quotes need a defined LCD, sensor and controller boundary. touch display module scope.
6. Which defects need a shared inspection method?
Define relevant bubbles, particles, edge appearance, misalignment and display artifacts in terms the project can inspect. Meanwhile, visibility changes with lighting, content and angle. Separate cosmetic limits from functional failures and identify the viewing area. A generic zero-defect phrase without a method is less useful than a reproducible acceptance standard.
Receiving and factory teams can disagree about the same feature. Uncontrolled photographs may exaggerate or conceal a visible defect.
What failure would reject this configuration?
Make defects consistently inspectable. Agree on inspection conditions and applicable limits before the pilot. Retain identified reference samples or controlled records, then use the same method for factory release, receiving and failure review.
- Defect categories
- Viewing area
- Inspection setup
- Acceptance limits
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | Receiving and factory teams can disagree about the same feature. Uncontrolled photographs may exaggerate or conceal a visible defect. | Inspection setup |
| Approval action | Agree on inspection conditions and applicable limits before the pilot. Retain identified reference samples or controlled records, then use the same method for factory release, receiving and failure review. | Acceptance limits |
Review the capacitive product context if glass-front or gesture operation enters the specification. capacitive touchscreen options.
7. Does optical joining define touch performance?
Touch operation still depends on the sensor, cover, controller, firmware and host. The joined stack can change the configuration that needs evaluation. Also, display activity and nearby electronics may affect sensing. A visually successful bond should therefore receive relevant input testing rather than being treated as proof of gesture, glove or moisture capability.
An optical pass can coexist with poor input or host mapping. Tuning one operating state may alter another required condition.
What should quality retain?
Keep optical and input gates separate. Test representative tasks and idle behavior on the complete configuration. Retain controller and host references, then repeat affected states after stack, firmware or mounting changes.
- Sensor reference
- Controller revision
- Host behavior
- Input matrix
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An optical pass can coexist with poor input or host mapping. Tuning one operating state may alter another required condition. | Host behavior |
| Approval action | Test representative tasks and idle behavior on the complete configuration. Retain controller and host references, then repeat affected states after stack, firmware or mounting changes. | Input matrix |
Use the pressure-input product context when a suitable blunt stylus or glove is required. resistive touchscreen options.
8. What mechanical consequences require review?
Joining couples layers that previously could have different movement paths. Material properties, thickness and mounting affect stress transfer. Meanwhile, boards, tails and frame joints remain separate failure points. Do not translate optical coupling into a universal impact or vibration claim. Evaluate the installed load path and relevant exposure requirements through qualified engineering owners.
A stronger-looking stack can still be constrained poorly. Material evidence cannot qualify an unrelated frame, connector or enclosure.
Which trial result changes the decision?
Trace loads beyond the adhesive. Review support and clearance references with the mechanical team. Define relevant tests for the complete assembly, then inspect both optical condition and functional behavior before and after the approved exposure plan.
- Layer coupling
- Mounting support
- Interconnects
- Test scope
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | A stronger-looking stack can still be constrained poorly. Material evidence cannot qualify an unrelated frame, connector or enclosure. | Interconnects |
| Approval action | Review support and clearance references with the mechanical team. Define relevant tests for the complete assembly, then inspect both optical condition and functional behavior before and after the approved exposure plan. | Test scope |
A bonding proposal changes the assembled optical and mechanical interface; review its construction context. fully laminated touchscreen construction.
For example, a buyer might receive two optical-bonding offers: one joins only the cover and sensor, while another also couples the sensor to the LCD. Draw both sections before comparing the samples or fee. Then evaluate the required visual and input tasks on the intended complete assembly. This hypothetical example shows why identifying the treated interface matters more than accepting a broad process label.
9. How does the process affect repair ownership?
Removing a joined layer can require specialist equipment and may damage parts. The outcome depends on the actual construction and approved process. Also, reworked parts need defined inspection before reuse. Decide who owns incoming defects, process scrap and replacement scope rather than assuming that every joined LCD remains economically recoverable.
An unqualified separation attempt can increase loss. A quote may omit the risk attached to customer-supplied high-value parts.
How can purchasing compare the evidence?
Clarify recovery before ordering. Request the approved rework boundary and loss-allocation rules. Compare full-module replacement with any qualified recovery route, then retain reinspection and traceability requirements for returned or repaired assemblies.
- Rework scope
- Part-loss owner
- Replacement route
- Reinspection rules
| Decision point | Requirement to retain | Related check |
|---|---|---|
| Failure boundary | An unqualified separation attempt can increase loss. A quote may omit the risk attached to customer-supplied high-value parts. | Replacement route |
| Approval action | Request the approved rework boundary and loss-allocation rules. Compare full-module replacement with any qualified recovery route, then retain reinspection and traceability requirements for returned or repaired assemblies. | Reinspection rules |
For a machine installation, relate these checks to mounted-console and operator conditions. industrial control touchscreen context.
10. How should an OEM approve optical bonding?
Approve a defined stack and process output with identified evidence. Keep optical, input, installed mechanical and service decisions visible. By contrast, what is optical bonding is only the opening question; repeat supply requires controlled references. Material or geometry changes should trigger the checks affected by the proposed alteration, not an automatic assumption of equivalence.
A category-level order can permit a different construction. A process change may invalidate evidence even when the front looks similar.
What should the team release next?
Approve a reproducible construction. Release the accepted materials, drawings, process and inspection references together. Require relevant change notices and sample identity, then repeat affected checks before accepting substitutions or expanded operating conditions.
- Stack identity
- Process reference
- Acceptance evidence
- Change triggers
Frequently asked questions about what is optical bonding
Q1: Is optical bonding a display technology? It describes optical joining at selected interfaces, not a substitute name for the LCD or sensor technology.
Q2: Does it remove every reflection? No. Front-surface glare and other stack behavior remain relevant to the complete visual result.
Q3: Must every process use liquid adhesive? No. Suitable films, liquid systems and other qualified approaches depend on the proposed construction.
Q4: Does a good optical bond prove glove input? No. Verify the assembled sensor, controller, host and defined glove conditions separately.
Q5: What should a purchase approval identify? The accepted stack, materials, process output, inspection method and change rules.